Maximum process control with ultrapure water

Demineralised water for the chemical industry

Water is often a crucial raw material in chemical production processes. Its quality directly affects chemical reactions, product quality, process safety and equipment reliability. A professional demineralisation system provides a constant source of demineralised water, allowing you to control your processes effectively.

Why use demineralised water in the chemical industry?

Precision, process control and consistent product quality are vital in the chemical industry. Even small amounts of dissolved salts, minerals or other contaminants can affect chemical reactions and cause deviations in the final product. Tap water naturally contains substances such as calcium, magnesium, chlorides and sulphates, whose concentrations may vary. Untreated tap water is therefore not always suitable for chemical production processes.

Demineralised water is water from which almost all dissolved salts and minerals have been removed. It provides a reliable basis for processes in which precise water composition is essential. Using demineralised water reduces the risk of unwanted chemical reactions, contamination and deviations from product specifications. This contributes to consistent product quality, fewer rejected batches and more efficient production.

Demineralised water also helps prevent limescale deposits in pipes, tanks and production equipment. Systems stay cleaner, maintenance requirements decrease and the risk of faults and unplanned production downtime is reduced.

Consistent water quality is essential. Fluctuations in process water composition can disrupt the reproducibility of chemical reactions and lead to production losses or higher operating costs. A professional demineralisation system continuously provides water with stable, low conductivity, tailored to your production requirements.

For chemical manufacturers, this means greater control over production, a lower risk of rejected batches, lower maintenance costs and more reliable results. High-quality water treatment provides an important foundation for efficient, consistent production.
The benefits of demineralised water

Consistent and controlled water quality
Optimal process control
Improved product consistency
Reduced risk of contamination
Less limescale and corrosion
Lower maintenance costs
Greater process reliability
Longer equipment service life
Fewer rejected products and production losses

Applications of demineralised water in the chemical industry

Process water for chemical production

Demineralised water is used as a raw material or process water in the production of chemicals, coatings, adhesives, polymers, plastics and speciality chemicals. Consistent water quality prevents unwanted variations in product compositions and process results.

Dissolving and mixing chemicals

Demineralised water allows raw materials to be dosed precisely without interference from minerals or salts present in tap water.

Cleaning equipment

Production tanks, reactors, pipework and mixing systems need regular cleaning. Demineralised water prevents limescale and residual contaminants, making cleaning processes more effective.

Boiler feedwater and steam generation

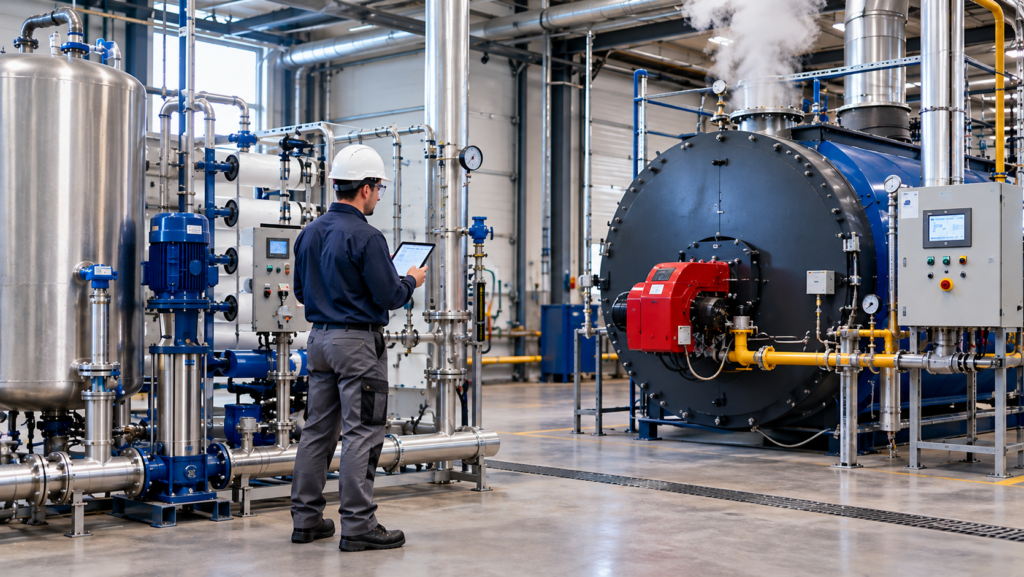
Many chemical companies use steam in production. Demineralised water prevents deposits in boilers and pipework, allowing equipment to work more efficiently and reducing maintenance.

Cooling water and process cooling

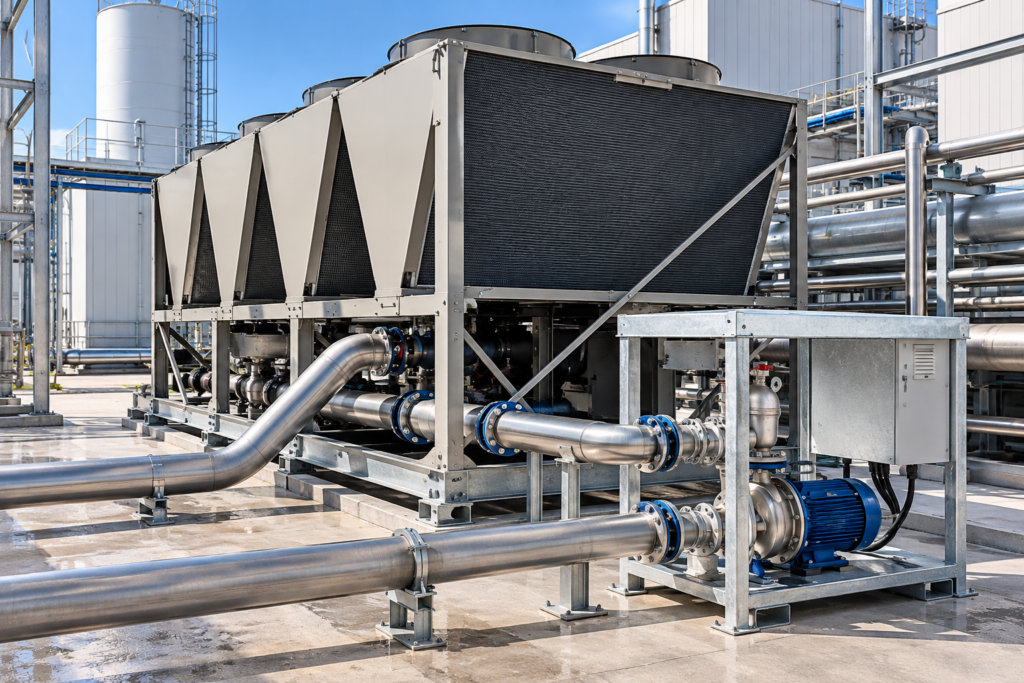
In cooling circuits, demineralised water helps minimise limescale, corrosion and fouling. This improves the reliability of heat exchangers, chillers and cooling systems.

Why choose FDS Waterbehandeling?

Reliable and sustainable water treatment for the chemical industry

Consistent water quality is essential for reliable and efficient chemical production. A professional demineralisation system prevents unwanted fluctuations in water composition and reduces the risk of fouling, limescale and rejected products. This contributes to consistent product quality, less maintenance and greater process reliability. Tailoring water purification precisely to your production process also allows you to optimise water consumption and make better use of opportunities to reuse process water.

With more than 20 years of experience, FDS Waterbehandeling understands the chemical industry’s water quality requirements. Our high-quality demineralisation systems are tailored to your specific production process and provide reliable water for applications ranging from bulk and speciality chemicals to coatings, plastics and paint production.

Our systems are built using carefully selected, high-quality components. We supply reliable, easy-to-maintain systems with a long service life and optimal performance, even under intensive industrial use.

Looking for a demineralisation system for the chemical industry?

Would you like greater control over your process water and to protect your production environment from contaminated or mineral-rich water? Our specialists will be happy to advise you on the best demineralisation system for your production process, water consumption and quality requirements.

Request advice with no obligation